Case-hardening response
Carbon can be introduced at the surface and followed by quenching and tempering to create high surface hardness while retaining lower-carbon core behavior.
Custom 8620 alloy steel machining in China
We manufacture custom CNC machined 8620 steel parts from customer drawings, 3D models, physical samples and functional requirements. Our 8620 CNC machining service supports precision shafts, gears, pinions, splined components, sleeves, hubs, bushings and other wear-resistant alloy steel parts. Production can be arranged from one prototype or replacement component through low-volume batches and repeat mass production.
AISI 8620 is especially valuable when a component needs two different behaviors: a hard, wear-resistant case and a comparatively tough core. CNC turning, CNC milling, drilling, boring, reaming, threading, spline machining, gear-related features, heat-treatment allowance, finish grinding and dimensional inspection can be coordinated around the final drawing requirements.
Material overview
SAE 8620 is a low-carbon nickel-chromium-molybdenum alloy steel widely selected for carburized mechanical parts. The alloy combines useful machinability before heat treatment with the hardenability required to produce a durable case and a load-bearing core.
Carbon can be introduced at the surface and followed by quenching and tempering to create high surface hardness while retaining lower-carbon core behavior.
The hardened case can resist sliding wear, rolling contact stress and repeated tooth or spline engagement in power-transmission components.
Nickel, chromium and molybdenum improve hardenability and help the core carry shock and bending loads after an appropriate heat-treatment cycle.
Most material removal is completed in the annealed, normalized or supplied condition, with planned stock left only where post-heat-treatment finishing is needed.
Related products
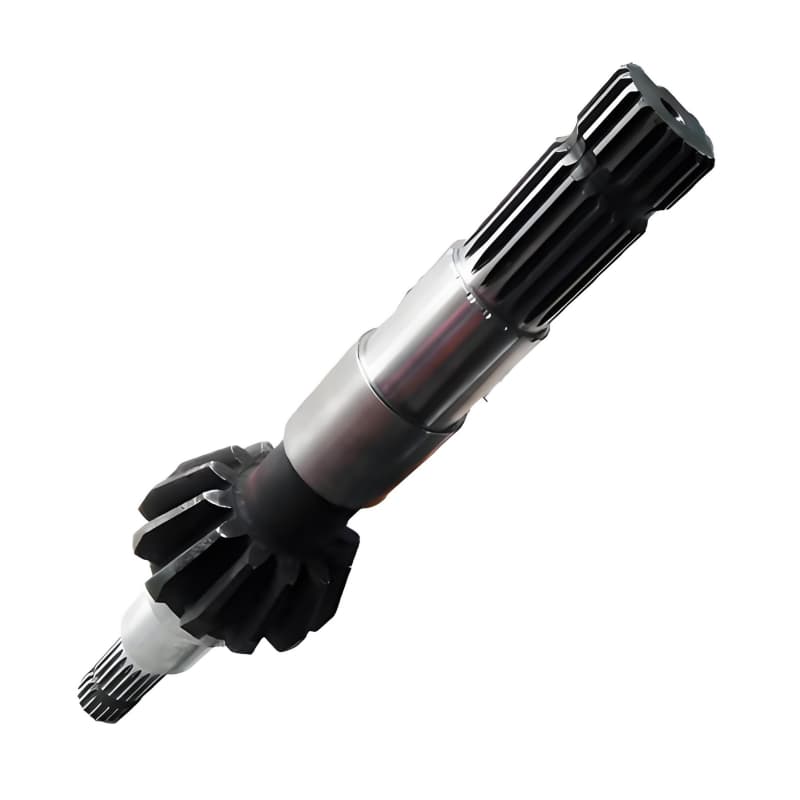
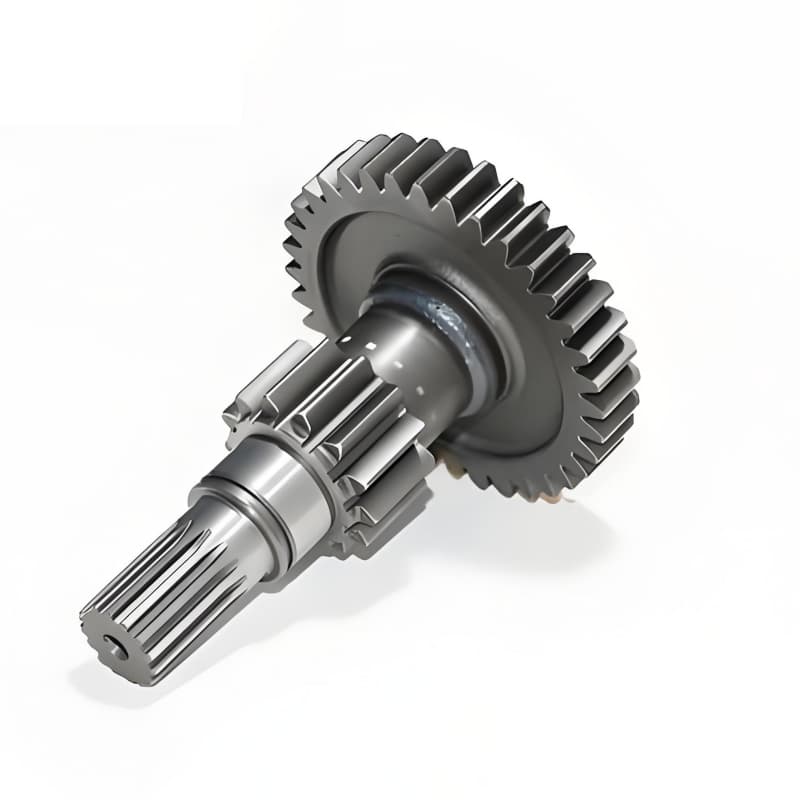
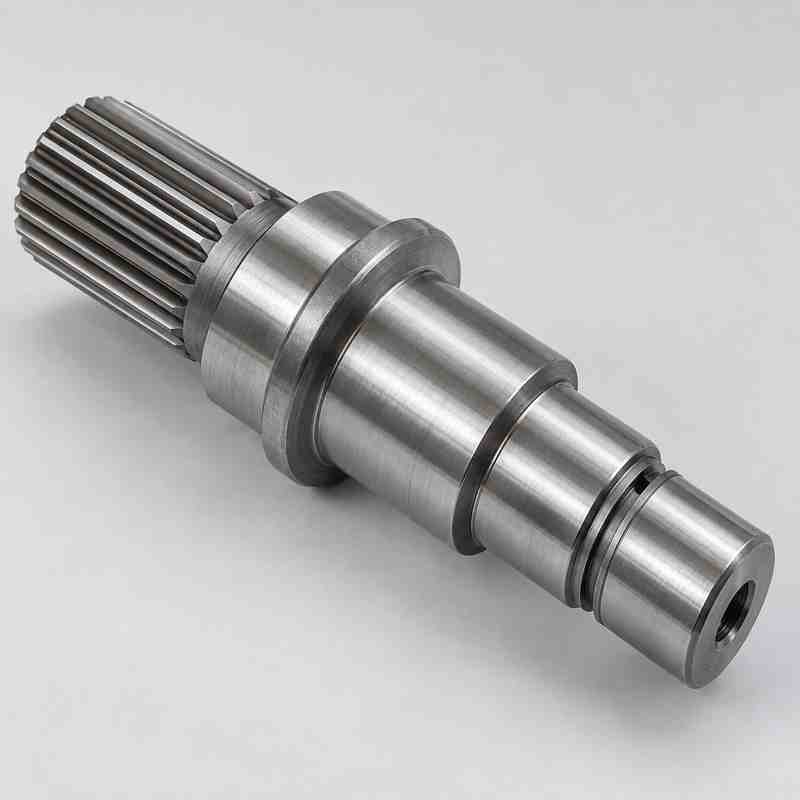
Representative OEM steel components include splined shafts, gear-and-shaft assemblies, cutting components and precision transmission parts. Every production part is made to the geometry, tolerance, heat-treatment and surface requirements stated on the customer drawing.

Composition and performance
Alloy composition, starting condition, section size, carburized case depth, quench severity and tempering cycle all influence the final result. Drawing requirements should therefore separate raw-material chemistry, core properties, case hardness, effective case depth and finished dimensions.
| Element | Typical SAE 8620 range by weight | Practical influence |
|---|---|---|
| Carbon | 0.18–0.23% | Supports machinability in the core and allows a high-carbon case to be created by carburizing. |
| Manganese | 0.70–0.90% | Contributes to strength and hardenability. |
| Silicon | 0.15–0.35% | Functions as a deoxidizer and contributes modestly to strength. |
| Nickel | 0.40–0.70% | Supports toughness, especially in the load-bearing core. |
| Chromium | 0.40–0.60% | Improves hardenability, wear behavior and carbide formation in the case. |
| Molybdenum | 0.15–0.25% | Improves hardenability and helps maintain useful core strength. |
| Phosphorus | 0.040% maximum | Controlled as a residual element because excess content can reduce toughness. |
| Sulfur | 0.035% maximum | Controlled to balance machinability and mechanical performance. |
Chemical ranges are typical reference values for SAE 8620. The purchase specification, applicable product standard, bar or forging condition and actual heat analysis must govern production. A grade name alone does not define final mechanical properties.
Typical density is approximately 7.8–7.9 g/cm³ and elastic modulus is approximately 200–210 GPa, similar to many engineering alloy steels.
A carburized, quenched and tempered case is commonly specified around 58–62 HRC, but the drawing and heat-treatment specification must define the acceptable range.
Core hardness, tensile strength and impact behavior depend strongly on section size, material hardenability and the exact thermal cycle.
Effective case depth is selected from contact stress, wear allowance and component size. Values around 0.5–1.5 mm are common, but thinner or deeper cases may be specified.
8620 machines well in a softer supplied condition. Stable workholding, controlled tool load and appropriate cutting data help maintain concentricity and tooth-location accuracy.
Carburizing and quenching can move bores, faces, splines and long shafts. Process planning must anticipate distortion rather than treating heat treatment as a final cosmetic step.
The low carbon level can permit welding with a controlled procedure, but welding near carburized or finish-hardened surfaces is generally avoided unless engineering approval is provided.
8620 is not stainless steel. Oil, conversion coating, plating, paint or another corrosion-control system may be required for storage and service exposure.
Cross-standard comparison
International designations are frequently compared during global sourcing, but they are not automatically interchangeable. Chemistry limits, hardenability bands, cleanliness requirements, product form, grain size and heat-treatment response must be checked before substitution.
| Country or system | Common designation | Relationship to SAE 8620 | Engineering note |
|---|---|---|---|
| United States | SAE/AISI 8620; UNS G86200 | Primary American designation used for the material on this page. | 8620H is a hardenability-controlled variant and should not be assumed identical to ordinary 8620 without review. |
| European EN | 20NiCrMo2-2; material number 1.6523 | Frequently cross-referenced European case-hardening grade with closely overlapping alloy content. | Confirm the applicable EN product standard and compare every chemistry limit on the drawing or purchase specification. |
| United Kingdom | 805M20 | Commonly cited British comparison for a low-carbon Ni-Cr-Mo case-hardening steel. | Legacy and current specifications may differ; verify revision, condition and hardenability requirements. |
| Japan | JIS SNCM220 | Common Japanese comparison with similar carbon, nickel, chromium and molybdenum ranges. | Use the current JIS specification and approve substitution from a direct composition and property comparison. |
| China | GB/T 3077 20CrNiMo | Common Chinese alternative used for gears, shafts and other carburized parts. | Some manganese, chromium, nickel and molybdenum limits differ from SAE 8620, so it is a related grade rather than a universal drop-in replacement. |
For custom 8620 steel parts, the safest drawing practice is to state the required standard and revision, permitted alternatives, raw-material condition, hardenability requirement if applicable, core hardness, case hardness and effective case depth. Substitution should be approved before material is cut.
Manufacturing capability
The manufacturing route is chosen from geometry, annual quantity, datum structure, heat-treatment condition and the relationship between critical features. Combining operations in stable setups can reduce accumulated error and improve repeatability.
Outside diameters, shoulders, tapers, grooves, seal lands, threads, bores and end faces for shafts, hubs, sleeves, rollers and bushings.
Flats, pockets, keyways, slots, mounting faces, hole patterns and prismatic features on blocks, hubs and transmission components.
Indexed radial holes, circumferential features, multiple keyways and milled profiles around shafts with fewer datum transfers.
Compound-angle holes, complex faces and multi-sided geometry where controlled access and fewer setups improve feature relationships.
External or internal tooth and spline features can be planned by milling, hobbing, shaping, broaching or wire EDM according to geometry and volume.
Drilling, boring, reaming, spot-facing and counterboring produce assembly holes, bearing seats, dowel locations and oil passages.
Wire EDM or sinker EDM may be used for sharp internal details, narrow slots, hardened profiles or features that are inefficient to cut conventionally.
Cylindrical grinding, surface grinding, honing, hard turning or selective polishing can restore critical dimensions after heat treatment.
Carburizing-aware production
A good process plan begins with the final hardened geometry. Case depth, masked areas, grinding stock, stock-removal limits and distortion risk are decided before rough machining, not after the parts leave heat treatment.
Identify surfaces that require hardness, the effective case-depth criterion, permitted soft areas and any hardness transition requirements.
Establish centers, faces, bores and reference surfaces that can be reused through roughing, finishing and final inspection.
Reserve material on bearing journals, seal diameters, precision faces or bores that will be ground or hard-finished after carburizing.
Threads, weld areas, centers, deep holes or features that must remain machinable may require masking or copper plating under the heat-treatment plan.
A process-specific thermal cycle develops the specified case and core. Fixture method, load arrangement and quench control influence distortion.
Critical features are ground or hard-finished, then checked for size, form, location, surface texture and specified hardness or case-depth results.
Accuracy and finish
Achievable values depend on feature size, length-to-diameter ratio, wall thickness, datum access, material condition, heat treatment, quantity and inspection method. The ranges below are realistic planning references, not universal limits for every 8620 part.
| Feature or process | Typical planning capability | Important conditions |
|---|---|---|
| General CNC turned or milled dimensions | Often ±0.05 mm | Suitable for many non-critical dimensions before heat treatment. |
| Precision machined dimensions | Often ±0.01–0.02 mm | Requires stable geometry, controlled setup, appropriate tool access and matched inspection. |
| Ground journals and selected diameters | Approximately ±0.003–0.008 mm where geometry permits | Normally completed after heat treatment; roundness and cylindricity must be specified separately when functional. |
| Precision bores | H7 or drawing-specific limits may be achievable | Method may include boring, reaming, honing or internal grinding according to size and condition. |
| Position, runout and concentricity | Drawing-specific geometric tolerances | Results depend on datum design, setup sequence, section rigidity and whether features are measured before or after hardening. |
| Standard CNC turned or milled finish | Commonly Ra 1.6–3.2 µm | Tool path, feed, insert geometry, stock condition and feature accessibility affect texture. |
| Fine machined finish | Commonly Ra 0.8–1.6 µm | Applicable to selected accessible surfaces with a dedicated finish operation. |
| Ground or honed finish | Commonly Ra 0.2–0.8 µm | The process is selected from functional directionality, size, form tolerance and stock allowance. |
Heat treatment and surface protection
Case hardening changes mechanical performance; coatings and conversion finishes mainly change corrosion behavior, appearance, friction or break-in performance. The sequence must account for masking, hydrogen-embrittlement risk, dimensional buildup and post-treatment grinding.
The principal treatment for 8620 gears, pinions, shafts and wear surfaces requiring a hard case over a tough core.
A shallower case-hardening option for selected small parts when the drawing and service conditions call for it.
A thin dark conversion finish used for appearance and light corrosion protection when paired with oil or wax.
Zinc or manganese phosphate can support oil retention, running-in behavior, paint adhesion or temporary corrosion protection.
Provides sacrificial corrosion protection; coating thickness, masking and post-plating treatment must suit the hardened part.
Offers relatively uniform coverage and improved corrosion or wear behavior, with dimensional buildup included in final limits.
Can introduce compressive surface stress on specified regions to support fatigue performance when the process is properly controlled.
Suitable for non-fitting external areas that need color and environmental protection; threads, datums and fits are normally masked.
Typical applications
8620 is most useful where surface contact or wear is severe but the entire section should not become extremely hard and brittle. Part suitability still depends on load spectrum, geometry, lubrication, impact, case depth and core-property requirements.
End-use sectors
Custom 8620 components serve power transmission, motion systems and heavy-duty mechanisms where repeat contact, torque, shock and wear must be balanced against manufacturability and cost.
Differential parts, transmission components, hubs, shafts, pinions and other case-hardened drive elements.
Custom gears, splines, couplings, output shafts and compact power-transmission components.
Sprockets, shafts, pins and drivetrain parts exposed to impact, dirt and intermittent loading.
Wear-resistant mechanical components for drives, handling systems and rugged machinery assemblies.
Selected drive, coupling and tool components where the material and heat-treatment specification fits the service environment.
Rollers, hubs, sprockets and drive-system parts for conveyors, lifting systems and warehouse machinery.
Selected shafts, sleeves, gears and motion-transfer components outside unsuitable corrosive service.
Compact splined shafts, pinions, rotary elements and precision wear parts for repeated motion.
Machining and inspection
Inspection equipment is matched to the feature being controlled. Shop-floor checks support process stability, while optical and coordinate measurement are used for dimensions and geometric relationships that need more complete verification.
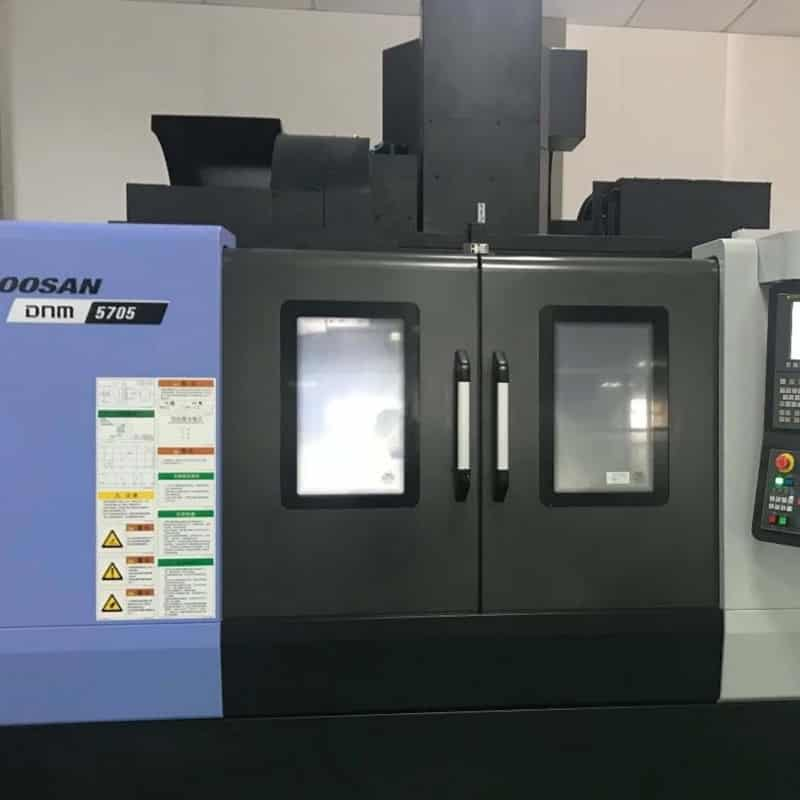
Controlled fixtures, datum planning and tool-path strategy support repeatable faces, pockets, slots and hole patterns.
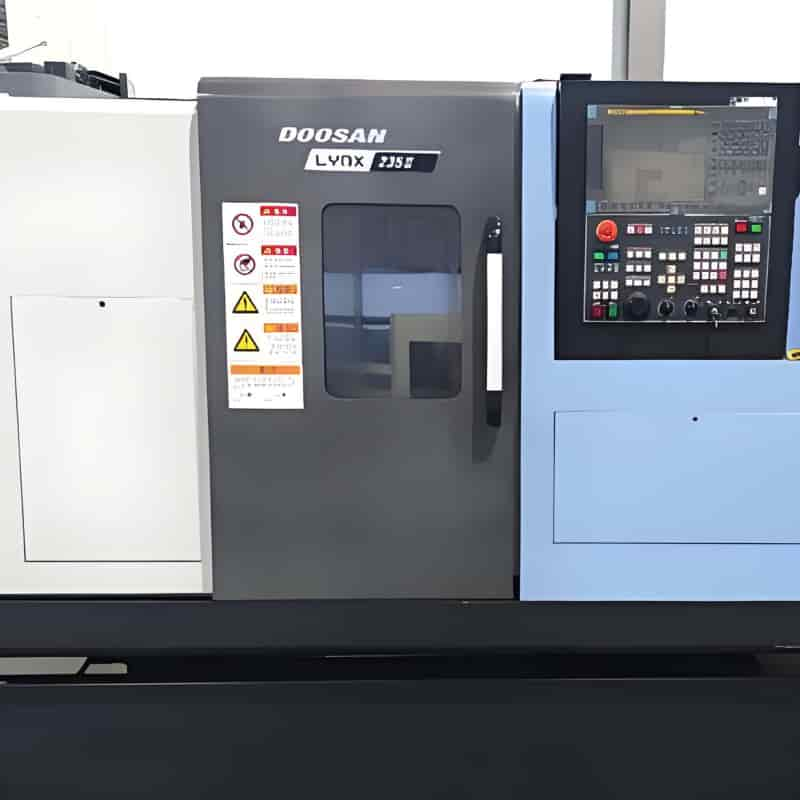
Turning operations establish functional diameters, shoulders, bores, threads and coaxial reference features.
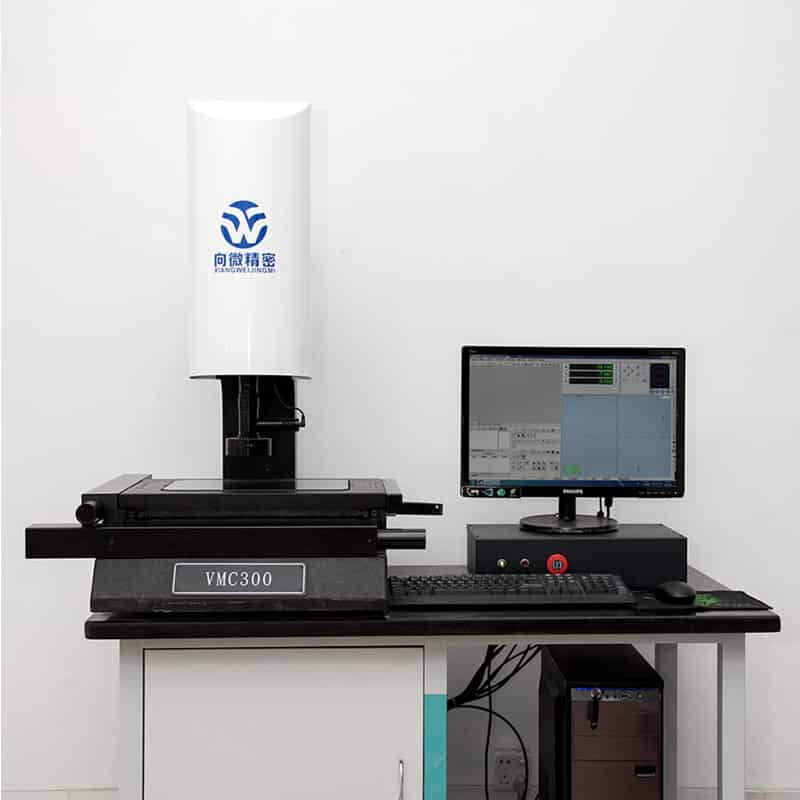
A 2D profile projector is useful for profiles, radii, edge features, angles and selected small-part dimensions.
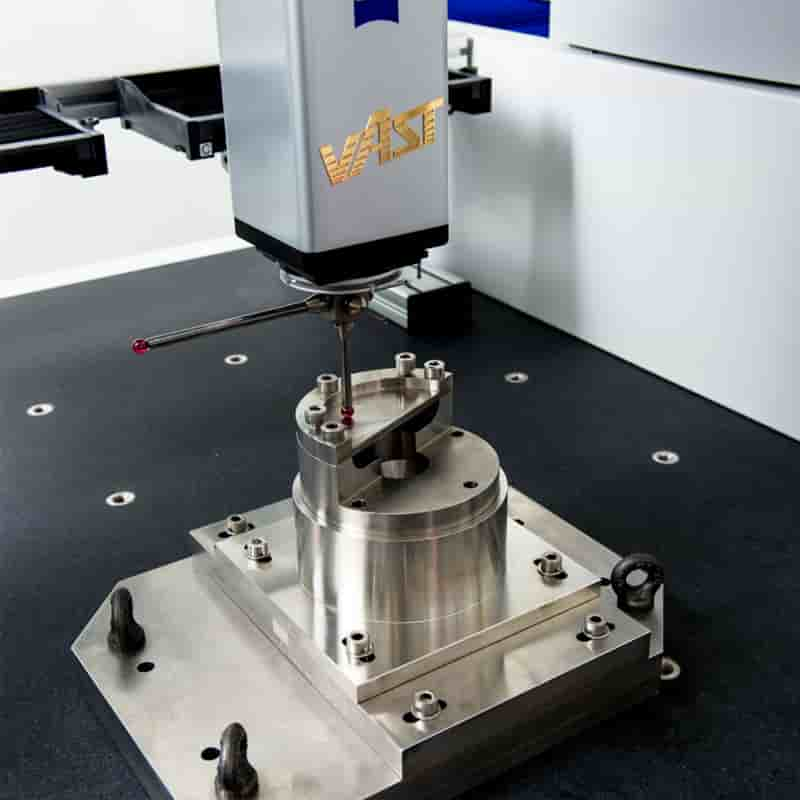
Coordinate measurement supports complex datum systems, hole locations, profiles and geometric relationships.
Grade, product form, starting condition and blank dimensions are reviewed against the manufacturing plan before machining begins.
Critical diameters, lengths, runout, tool wear and datum locations are monitored before value is added by later operations.
Feature-specific gauges or measurement methods can check fit, tooth thickness, runout, lead, profile or span dimensions as required.
Specified sealing, bearing and sliding surfaces can be evaluated with a roughness tester using the drawing’s parameter and cutoff requirement.
Surface and core hardness checks are coordinated with the heat-treatment requirement and the permitted test location.
Finished parts are evaluated in their required post-treatment condition, including coating or grinding where dimensions depend on those operations.
Drawing-to-production workflow
Prototype and volume production use the same engineering logic, but the fixture, inspection frequency, tool strategy and process controls are scaled to the quantity and repeat-order requirement.
Drawing, model, material, heat treatment, quantity and end-use priorities are checked together.
Datums, machines, setups, tooling, treatment sequence, finishing stock and inspection methods are defined.
Bar, tube, plate or forging is selected and cut with allowance for clamping, scale removal and machining.
Major stock is removed while leaving support and finish allowance where distortion or heat treatment matters.
Critical features are produced in a controlled sequence to manage location, runout and accumulated tolerance.
Carburizing or another specified cycle is completed with masking, test method and distortion considerations.
Grinding, honing, hard turning, deburring and protective finish are applied only where the drawing requires them.
Dimensions, geometry, surface texture and specified heat-treatment results are reviewed before packing.
Flexible order quantities
Order size changes the most economical route, but not the need for clear datums, controlled processes and measurable requirements. Production planning can evolve from a single validation part into fixtures and repeatable batch controls.
Replacement components, development hardware and special machine parts produced without a high minimum quantity.
Small quantities used to verify assembly, function, material choice, case-depth strategy and dimensional response.
Reusable workholding, planned tool life and defined in-process checks improve consistency and unit economics.
Dedicated fixtures, stable programs, controlled tool replacement and batch inspection support long-running requirements.
Engineering input
A complete technical package reduces assumptions, shortens process planning and helps the manufacturer choose the correct machining, heat-treatment and inspection route.
Material selection guidance
The best alloy is determined by the required property profile. A cross-standard equivalent matches a similar chemistry system; an alternative grade may solve the same design problem by a different heat-treatment route.
Choose 8620 when a carburized wear case and tough core are central. Consider 4140 when through-hardening, higher bulk carbon and general high-strength service are more appropriate.
9310 contains substantially more nickel and is often considered for more demanding core toughness and fatigue duty, with higher material and processing cost.
16MnCr5 is a widely used European case-hardening steel with a different alloy balance. It may suit gears and shafts, but it is not chemically identical to 8620.
8620 offers a strong case-hardening route but limited corrosion resistance. Select a suitable stainless grade when environmental resistance is the primary requirement.
Related search topics
The phrases below reflect common ways engineers and purchasing teams describe custom 8620 alloy steel machining, carburized parts, transmission components and international material comparisons.
Technical FAQ
These answers summarize the main design and purchasing questions for custom CNC machined 8620 steel parts. Final decisions must always follow the specific drawing and service conditions.
AISI 8620 is a low-carbon nickel-chromium-molybdenum alloy steel commonly used for carburized parts that need a hard, wear-resistant surface and a tougher core.
Yes. It is widely selected for gears, pinions, splines and other contact-loaded transmission parts. Tooth geometry, case depth, core strength, finish and lubrication must suit the load.
Most machining is normally completed before carburizing. Critical hardened dimensions may receive grinding, honing, hard turning or EDM after heat treatment.
A case hardness around 58–62 HRC is common with an appropriate carburize, quench and temper cycle. The exact range, test method and test location should be specified.
They are frequently cross-referenced because their alloy systems and chemistry ranges are similar. They should still be treated as comparable grades until the governing specifications are checked and substitution is approved.
GB/T 3077 20CrNiMo is a commonly used Chinese comparison. Its composition limits are not identical in every element, so the substitution must be reviewed against the drawing and performance requirements.
General CNC dimensions are often planned around ±0.05 mm, while selected stable features may reach ±0.01–0.02 mm. Ground features can be tighter. Geometry and heat-treatment distortion determine what is practical.
Standard CNC machining commonly produces Ra 1.6–3.2 µm, fine machining may reach Ra 0.8–1.6 µm, and grinding or honing can produce approximately Ra 0.2–0.8 µm on suitable features.
Yes. Manufacturing can begin with one prototype, repair or replacement part and then scale to low-volume or repeat production after fit and function are confirmed.
A controlled 2D PDF or DWG drawing plus a matching STEP, IGES or Parasolid model is ideal. Physical samples can also be used when drawings are incomplete, with critical requirements defined separately.
OEM alloy steel machining
Our China factory supports CNC machined 8620 steel parts for new product development, equipment replacement, low-volume industrial demand and repeat mass production. Material selection, machining sequence, carburizing allowance, final finishing and inspection are planned as one connected process so the finished component can meet its dimensional and functional requirements.