Specific PA Plastic Parts CNC Machining Service from China
We manufacture custom CNC machined PA parts directly from your engineering drawings, PDF/DXF/DWG files, STEP/IGES models or supplied samples. As a China-based PA plastic machining workshop, we produce CNC turned PA components and CNC milled PA components for machinery builders, automation lines, packaging equipment, food-grade conveying systems and engineering maintenance teams worldwide.
From a single PA machined prototype to repeated PA machined mass production parts, every nylon component is manufactured per drawing, with dimensions per drawing and tolerances per drawing kept under control on each production batch.
- CNC turning, CNC milling and combined turned & milled PA parts
- 3-axis, 4-axis and 5-axis machined PA parts for complex geometry
- PA6, PA66, PA66 GF30, PA12, PA46, cast nylon and oil filled PA stock
- Custom machined PA parts made per customer drawing or sample
- One-off pieces, prototypes, small batches and high-volume production
- Precision machined PA parts with full dimensional inspection records
Understanding Polyamide (PA / Nylon) as an Engineering Plastic
Polyamide, widely known as nylon, is one of the most frequently machined engineering thermoplastics. PA plastic machining is chosen whenever a part must combine mechanical toughness with low friction, good wear life and quiet operation - properties that metals often cannot deliver at the same weight and cost.
Material characteristics
PA offers high tensile and compressive strength, outstanding toughness under impact and repeated loading, excellent abrasion and wear resistance, natural self-lubrication and a low coefficient of friction. It dampens vibration and running noise, resists many oils, greases, fuels and weak chemicals, and weighs roughly one seventh of steel, which reduces inertia in moving assemblies. Glass filled PA grades further raise stiffness, load capacity and dimensional stability, while oil filled PA improves sliding behavior and extends wear life in dry-running positions.
Common stock colors
Extruded and cast PA stock is available in a range of standard colors, and custom colored sheet, rod and tube can be arranged for series production. Color never changes the way we machine the part - dimensions, tolerances and surface quality are controlled in exactly the same way regardless of pigment.
CNC machining performance
PA machines cleanly on standard CNC equipment with sharp tooling, high spindle speeds and controlled feed rates, producing tight chips and smooth, burr-free surfaces. Because nylon absorbs moisture and expands slightly with heat, we machine PA with sharp polished cutters, generous coolant-air flow, stress-relieved stock and stable clamping, then allow parts to condition before final inspection. This approach keeps PA turned parts and PA milled parts dimensionally stable and prevents warping in thin walls, deep pockets and long guide components.
Wear and abrasion resistance
PA withstands repeated sliding, rotating and scraping contact, which makes precision machined PA parts a common replacement for bronze, brass and mild steel wear components.
Mechanical toughness
Nylon absorbs shock and impact without cracking and keeps its strength under dynamic loads, an advantage for gears, cams, rollers and drivetrain components.
Self-lubricating, low friction
Natural lubricity - further improved in oil filled PA - allows PA bushings, sleeves and guide shoes to run with little or no external grease in many dry-running applications.
Noise and vibration damping
CNC machined PA gears, sprockets and star wheels run noticeably quieter than metal equivalents, softening meshing noise and absorbing vibration on high-speed machinery.
Chemical and oil resistance
PA stands up well to oils, greases, fuels, solvents and many industrial chemicals, suiting custom PA plastic components used inside gearboxes, hydraulic systems and process equipment.
Light weight and corrosion free
Low density cuts moving mass and energy consumption, while nylon never rusts, so PA milled parts serve reliably in humid, wash-down and chemically active environments.
Selected Custom Machined PA Parts in Production
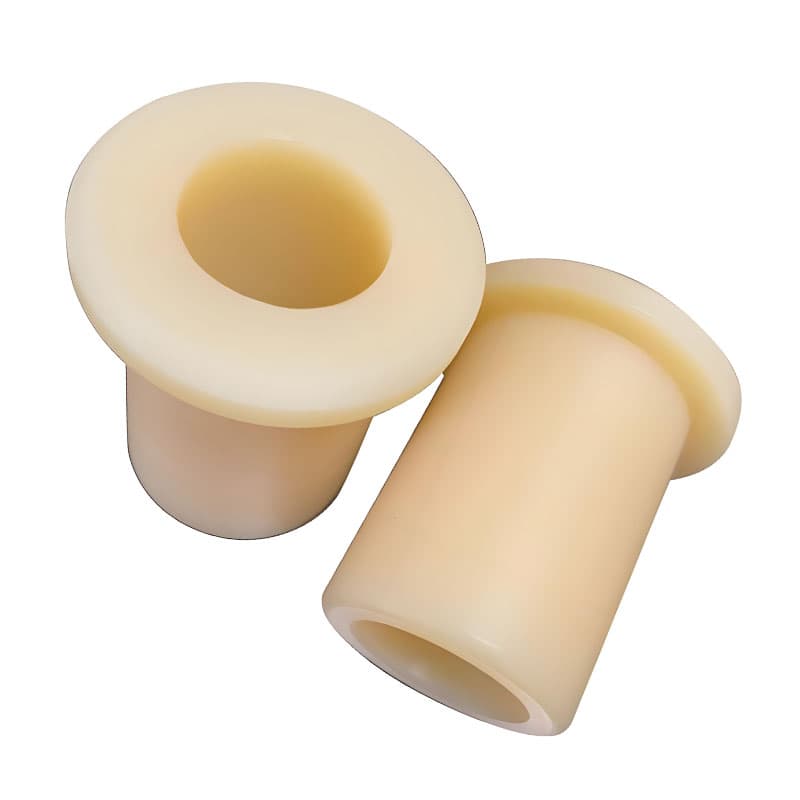
A quick look at typical nylon components machined on our floor - liners, transmission parts and custom PA66 machinery components, all built to customer drawings.


PA and Nylon Parts We CNC Machine Every Day
Custom machined PA parts cover a surprisingly wide range of shapes. Below are the most common nylon components we turn, mill and route from rod, plate, tube and cast nylon blanks, each produced as per engineering drawing.
CNC machined PA gears
Spur, helical, bevel and pinion gears with quiet meshing teeth for gearboxes, conveyors and office machinery.
CNC machined PA bushings
Plain and flanged nylon bushings and bearing sleeves for pivoting shafts, hinges and linkage points.
CNC machined PA rollers
Load, idler, guide and conveyor rollers turned from solid PA rod or machined around metal cores.
CNC machined PA wear pads
Wear strips, pads, shoes and slide blocks that protect metal rails under continuous friction.
CNC machined PA guide rails
Linear guide rails, chain guides and curved track sections milled from cast nylon plate.
CNC machined PA timing pulleys
Timing-belt pulleys, flat-belt pulleys and rope sheaves with accurate tooth profiles and bores.
CNC machined PA sprockets
Chain sprockets and star wheels for packaging, bottling and conveying lines that demand low noise.
CNC machined PA sleeves
Wear sleeves, spacer sleeves and reducer tubes CNC turned to close inner and outer diameter limits.
CNC machined PA spacers
Round and profile spacers, standoffs and distance tubes milled or turned to exact lengths.
CNC machined PA washers
Flat, shoulder and thrust washers that cushion contact faces and distribute clamping loads.
CNC machined PA flanges
Mounting flanges, bearing housings and bolt-circle flanges machined from solid nylon stock.
CNC machined PA cams
Plate cams, cam followers and indexing profiles milled with smooth, chatter-free contours.
CNC machined PA nuts
Full and half nuts, lead-screw nuts and trapezoidal nuts with self-lubricating internal threads.
CNC machined PA valve components
Valve seats, valve plates, sealing discs and manifold blocks for fluid and pneumatic equipment.
CNC machined PA seal retainers
Gland rings, seal housings and back-up rings that locate O-rings and lip seals precisely.
CNC machined PA mounting blocks
Brackets, clamping blocks and mounting bases that combine light weight with electrical insulation.
CNC machined PA insulating parts
Insulators, terminal plates and sensor holders for electrical and electronic assemblies.
CNC machined PA feed screws
Augers, dosing screws and feed screws with continuous helical flights for packaging and filling machines.
CNC machined PA scraper blades
Doctor blades, scraper strips and cleaner fingers that wipe belts and rolls without scratching them.
CNC machined PA guide wheels
Guide wheels, deflection rollers and U/V-groove wheels turned and grooved to match wire, rope or rail.
CNC machined PA conveyor parts
Side guides, transfer plates, chain tensioners and curved wear tracks for conveyor systems.
CNC machined PA jig components
Custom fixture jaws, locating pins, stop blocks and nest plates for production tooling and automation.
CNC machined PA handwheels
Knobs, grips, handwheels and operating levers turned and milled for ergonomic machine controls.
CNC machined PA custom blanks
PA machined blanks pre-shaped from plate or rod, ready for customers to finish in their own workshop.
PA Material Grades We Machine on Request
Choosing the right polyamide grade is part of the service. These are the high-frequency export grades we stock and machine; we always cut from the grade named on your drawing or specified in your purchase order.
PA6 machined parts
The general-purpose nylon grade with balanced strength, toughness and wear behavior. PA6 machined parts are the economical default for gears, rollers and wear components.
PA66 machined parts
Slightly stiffer, harder and more heat resistant than PA6, with excellent fatigue life for loaded, repeatedly cycled nylon machined components.
PA66 GF30 machined parts
PA66 reinforced with 30% glass fiber for high rigidity, creep resistance and dimensional stability in structural and high-load positions.
PA12 machined parts
The lowest-moisture nylon grade, dimensionally stable in humid conditions and well suited to precision parts, thin walls and fuel-contact components.
PA46 machined parts
A high-temperature polyamide that keeps strength and wear resistance where friction and continuous heat would soften standard nylon grades.
Cast PA / cast nylon
Cast nylon in large sheet, rod and tube formats delivers very high crystallinity and load capacity, ideal for big gears, sheaves and guide rails.
Oil filled PA
Nylon impregnated with lubricating oil for lifelong internal lubrication - the first choice for maintenance-free bushings and sliding wear parts.
Glass filled PA / GF PA
Glass-reinforced grades from GF15 to GF30 and above raise stiffness and temperature resistance for custom engineering plastic machining under load.
PA Plastic Machining Processes and Capabilities
Nylon turned & milled parts are produced on dedicated CNC equipment selected according to part geometry, batch size and tolerance demand - from simple PA turned parts to five-axis contoured components.
CNC turned PA components
Lathe work for rotational parts - bushings, rollers, sleeves, washers and nuts - with concentric bores, internal/external threads and fine turned finishes.
CNC milled PA components
3-axis and multi-axis milling for plates, blocks, guide rails, pockets, cams and contoured surfaces cut from PA sheet and cast nylon slab.
3-axis machined PA parts
Cost-efficient milling of flat and moderately complex custom machined PA parts where features are reached from three primary sides.
4-axis machined PA parts
Indexed rotary machining for parts with features around an axis, such as grooved rollers, cam drums and helical profiles in one setup.
5-axis machined PA parts
Simultaneous five-axis work for impeller-like shapes, compound angles and undercuts, reducing refixturing and preserving tight relationships.
PA machined prototypes
Fast turnaround of PA machined prototypes and first articles for fit checks, design verification and field testing before serial production.
PA machined blanks
Pre-cut and pre-machined PA machined blanks in rod, plate and tube form, stress-relieved and squared for customers doing secondary finishing.
PA machined mass production parts
Repeatable batch and series production with fixture-based machining, first-article approval and consistent quality across every delivery lot.
More PA Components We Turn and Mill to Drawing
The list below reflects real parts flowing through our PA plastic machining cells. If your component is not listed, send the drawing - most engineering plastic machined parts can be quoted directly from a dimensioned PDF or 3D model.
CNC machined PA parts by component name
Custom CNC machined PA parts built to your design
How PA Parts Are Machined and Measured
Stable machining processes and independent dimensional verification together ensure that every batch of nylon turned and milled parts matches the engineering drawing.
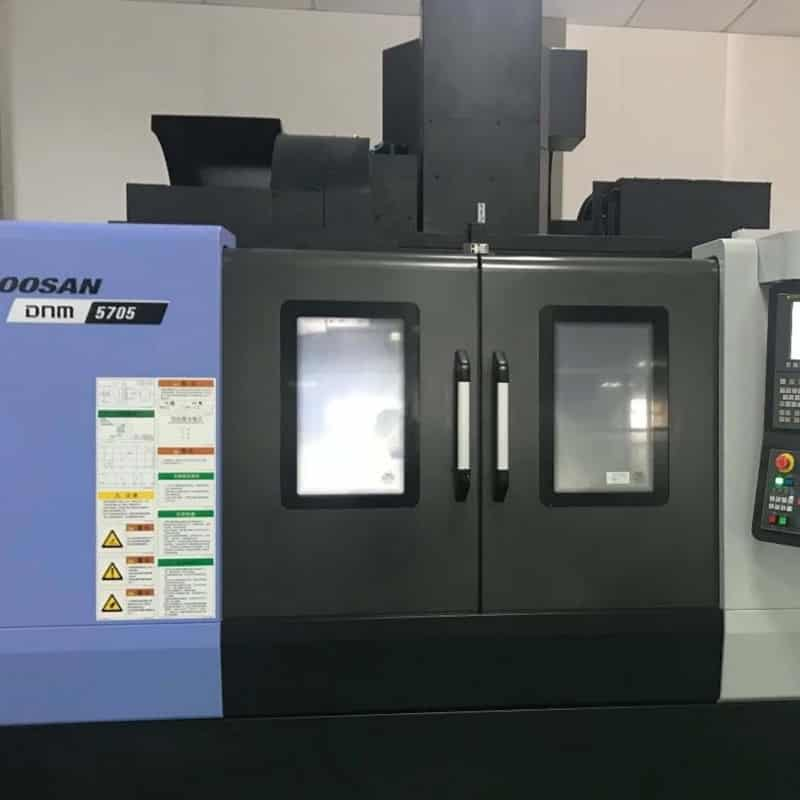
CNC milling
Vertical machining centers mill PA plates and blocks into guide rails, cams, fixtures and contoured custom nylon CNC parts.
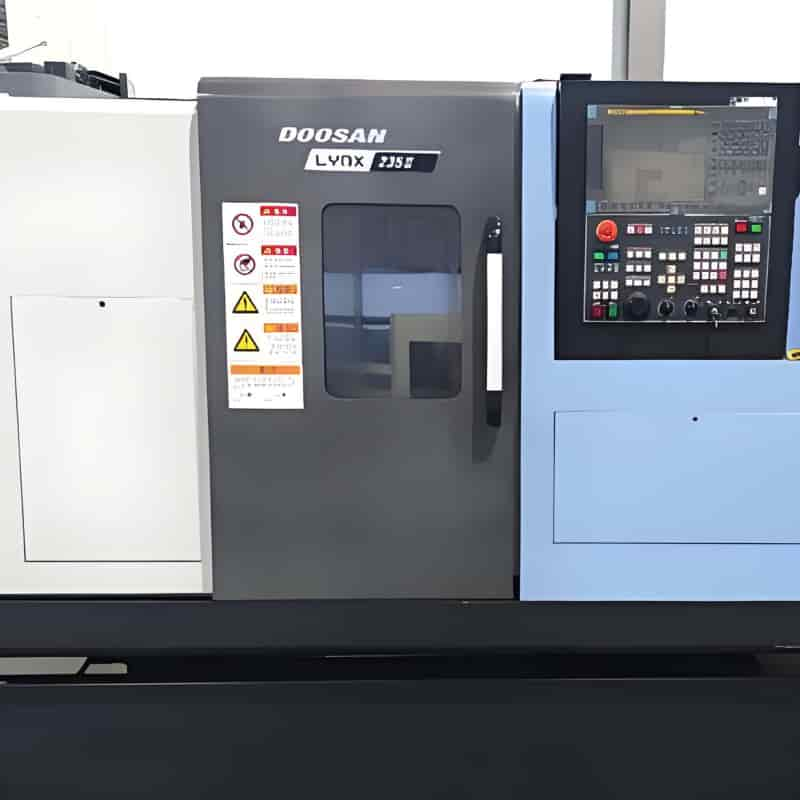
CNC turning
Precision lathes turn PA rod into concentric bushings, rollers, sleeves and threaded nylon components with fine surface finishes.
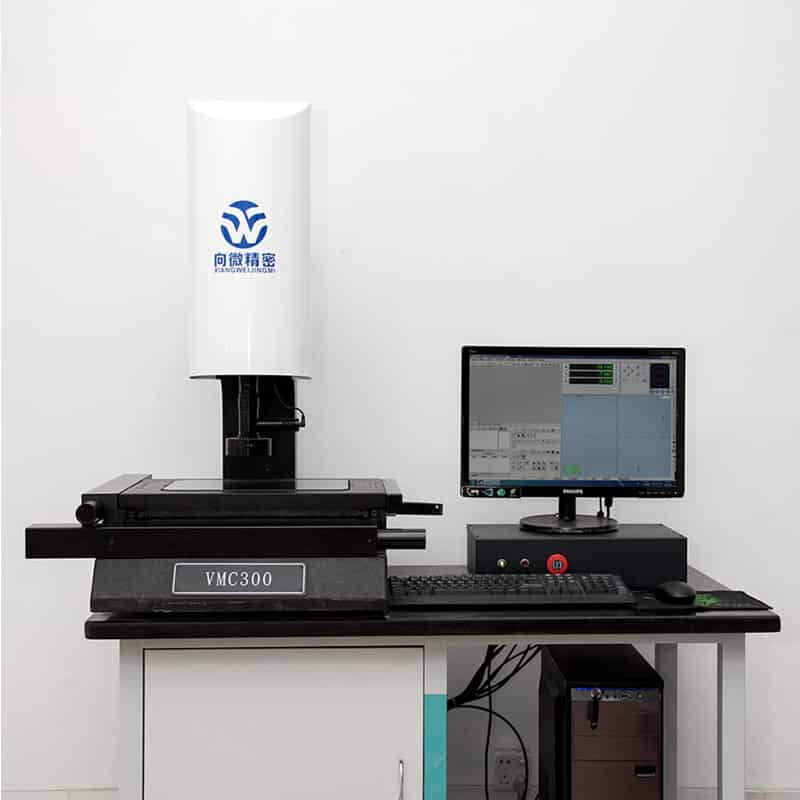
2D profile projection
An optical profile projector checks tooth forms, radii, angles and thin-wall profiles against the drawing's outline dimensions.
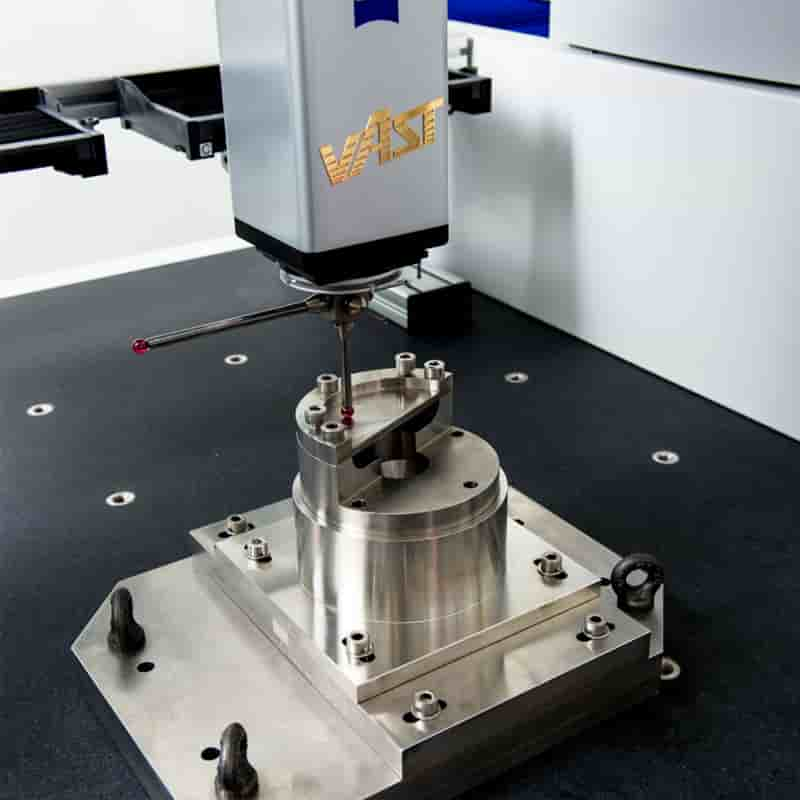
CMM inspection
A coordinate measuring machine verifies critical dimensions, positions and geometric tolerances on precision machined PA parts.
Surface Finish and Dimensional Accuracy on Machined PA
PA can be machined to a clean, precise and consistent result when tool geometry, feeds and material conditioning are controlled. The finish and accuracy we hold are always defined by your drawing - the values below describe typical shop-floor capability.
As-machined surface
Standard CNC machined PA parts leave the machine with a smooth, uniform matte surface, free of loose chips, frayed edges and tool chatter marks.
Fine turned and milled finishes
A typical machined nylon surface lands around Ra 1.6 to Ra 3.2 micrometers; with finishing passes, fine tooling and stable clamping, Ra 0.8-level surfaces can be reached on critical faces.
Dimensional tolerance per drawing
General features commonly hold within hundredth-of-a-millimeter ranges, and critical bores, fits and locating dimensions can be held tighter when the grade, wall thickness and geometry allow - always precision tolerance per drawing.
Geometric tolerances
Flatness, parallelism, perpendicularity, cylindricity, concentricity and position are controlled and verified as per engineering drawing call-outs.
Deburring and edge conditioning
Every part is deburred, with sharp edges broken, threads cleaned, bores blown clear and surfaces degreased so nylon components arrive ready to assemble.
Moisture and temperature control
Because PA absorbs moisture, parts are machined from stress-relieved stock, allowed to condition before final passes, and measured at stable shop temperature to limit post-machining movement.
Built Strictly Per Your Drawing
Our production and quality workflow follows the engineering document, not internal guesswork. The phrases below describe exactly how a custom PA plastic component moves from your file to a finished, inspected part.
Manufactured per drawing
Geometry, material, finish and quantity follow the released drawing or model, with no silent substitution of PA grade.
Dimensions per drawing
Every machined feature - bores, pitches, tooth counts, thicknesses - is taken directly from the dimensioned drawing.
Tolerances per drawing
General and bilateral tolerance blocks, as well as individually flagged limits, are applied feature by feature.
As per engineering drawing
Section views, thread specs, keyways, surface symbols and notes are treated as binding production instructions.
Per customer drawing
Customer-owned drawings and samples remain the single authority; sample-reverse parts are cross-checked with the customer.
Machined to drawing specification
Tool paths, setups and operation sequences are planned so the finished nylon part meets every specification on the sheet.
Precision tolerance per drawing
Critical fits and tight-tolerance features receive dedicated finishing passes and targeted measurement attention.
Inspection per drawing requirements
First-article and batch inspection check the dimensions and characteristics required by the drawing before release.
From a Single Piece to High-Volume Production
PA plastic machining is flexible by nature: there is no mold and no tooling investment, so the same drawing can be produced as one piece today and repeated in thousands later.
One-off and single pieces
A single replacement gear, bushing or wear rail machined from sample or sketch - common for machine maintenance and breakdown repairs.
PA machined prototypes
Small prototype runs for design validation, assembly trials and field testing, with fast iteration on dimension changes.
Small and medium batches
Tens to hundreds of custom nylon CNC parts produced with soft fixtures, first-article confirmation and lot-consistent quality.
Mass production parts
Repeated PA machined mass production parts in stable cycles, with dedicated fixturing, sampling plans and archived inspection records.
A China Workshop for Custom PA Plastic Components
When your equipment needs nylon parts that simply are not available off the shelf, custom engineering plastic machining is the fastest route from drawing to running machine.
Our workshop focuses on nylon machined components and the wider family of engineering plastic machined parts: custom nylon CNC parts in PA6, PA66, PA66 GF30, PA12, PA46, cast PA, oil filled PA and glass filled PA, produced by CNC turning, CNC milling and combined turn-mill processing. Whether the job calls for 3-axis machined PA parts, 4-axis machined PA parts or fully simultaneous 5-axis machined PA parts, each component is treated as a precision machined PA part: manufactured per drawing, machined to drawing specification and inspected per drawing requirements.
Nylon turned & milled parts from our floor include transmission and wear components - gears, sprockets, pulleys, bushings, rollers, guide rails, wear strips, cams, screws, valve components and custom machinery parts - as well as PA machined prototypes, PA machined blanks and PA machined mass production parts. We work from dimensioned drawings, 3D models or physical samples, and we support customers across the full quantity range, from a single custom machined PA part to recurring export batches of precision machined PA components made in China.